
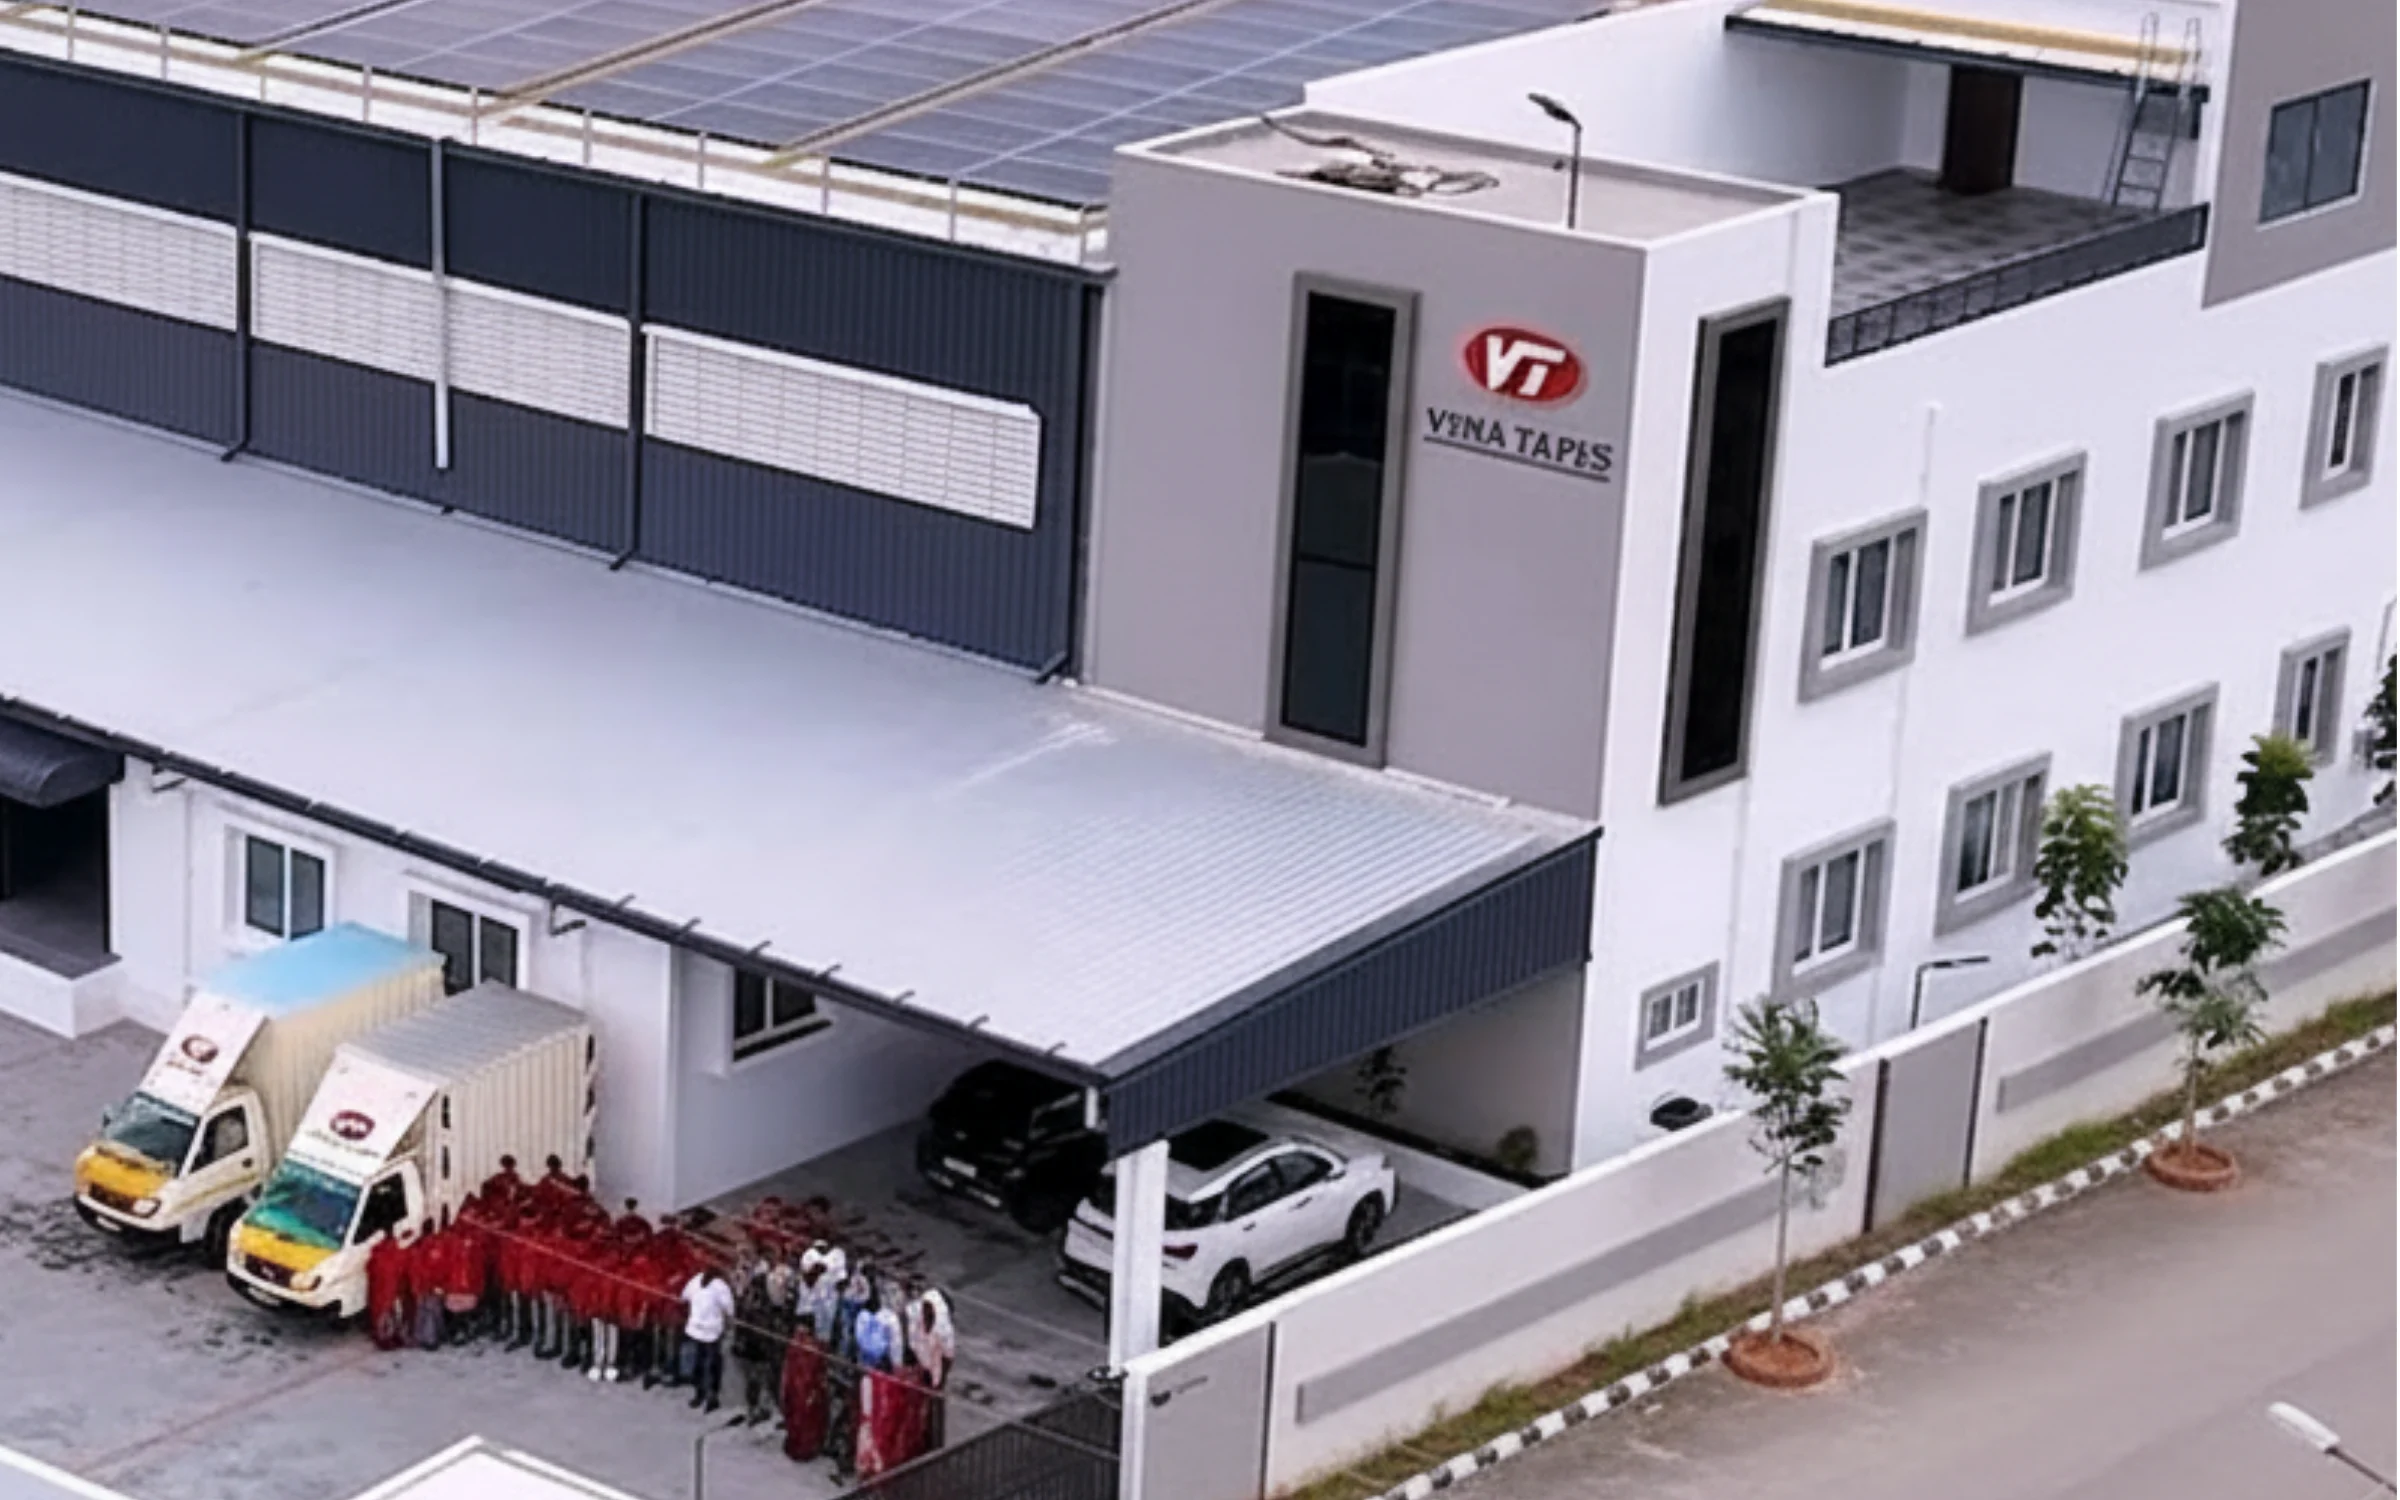
MANUFACTURING
- Spread across 40,000 sq. ft. of state-of-the-art manufacturing space, our facility is purpose-built for efficiency, precision, and high-volume production.
- Designed with modern workflows and advanced automation, it ensures seamless large-scale output while maintaining uncompromised quality at every stage.
- Our manufacturing capabilities are built around a streamlined production approach that combines precision, process control, and dependable output.
- Every stage is carefully managed to maintain uniformity in adhesive application, coating quality, roll formation, and final product performance.
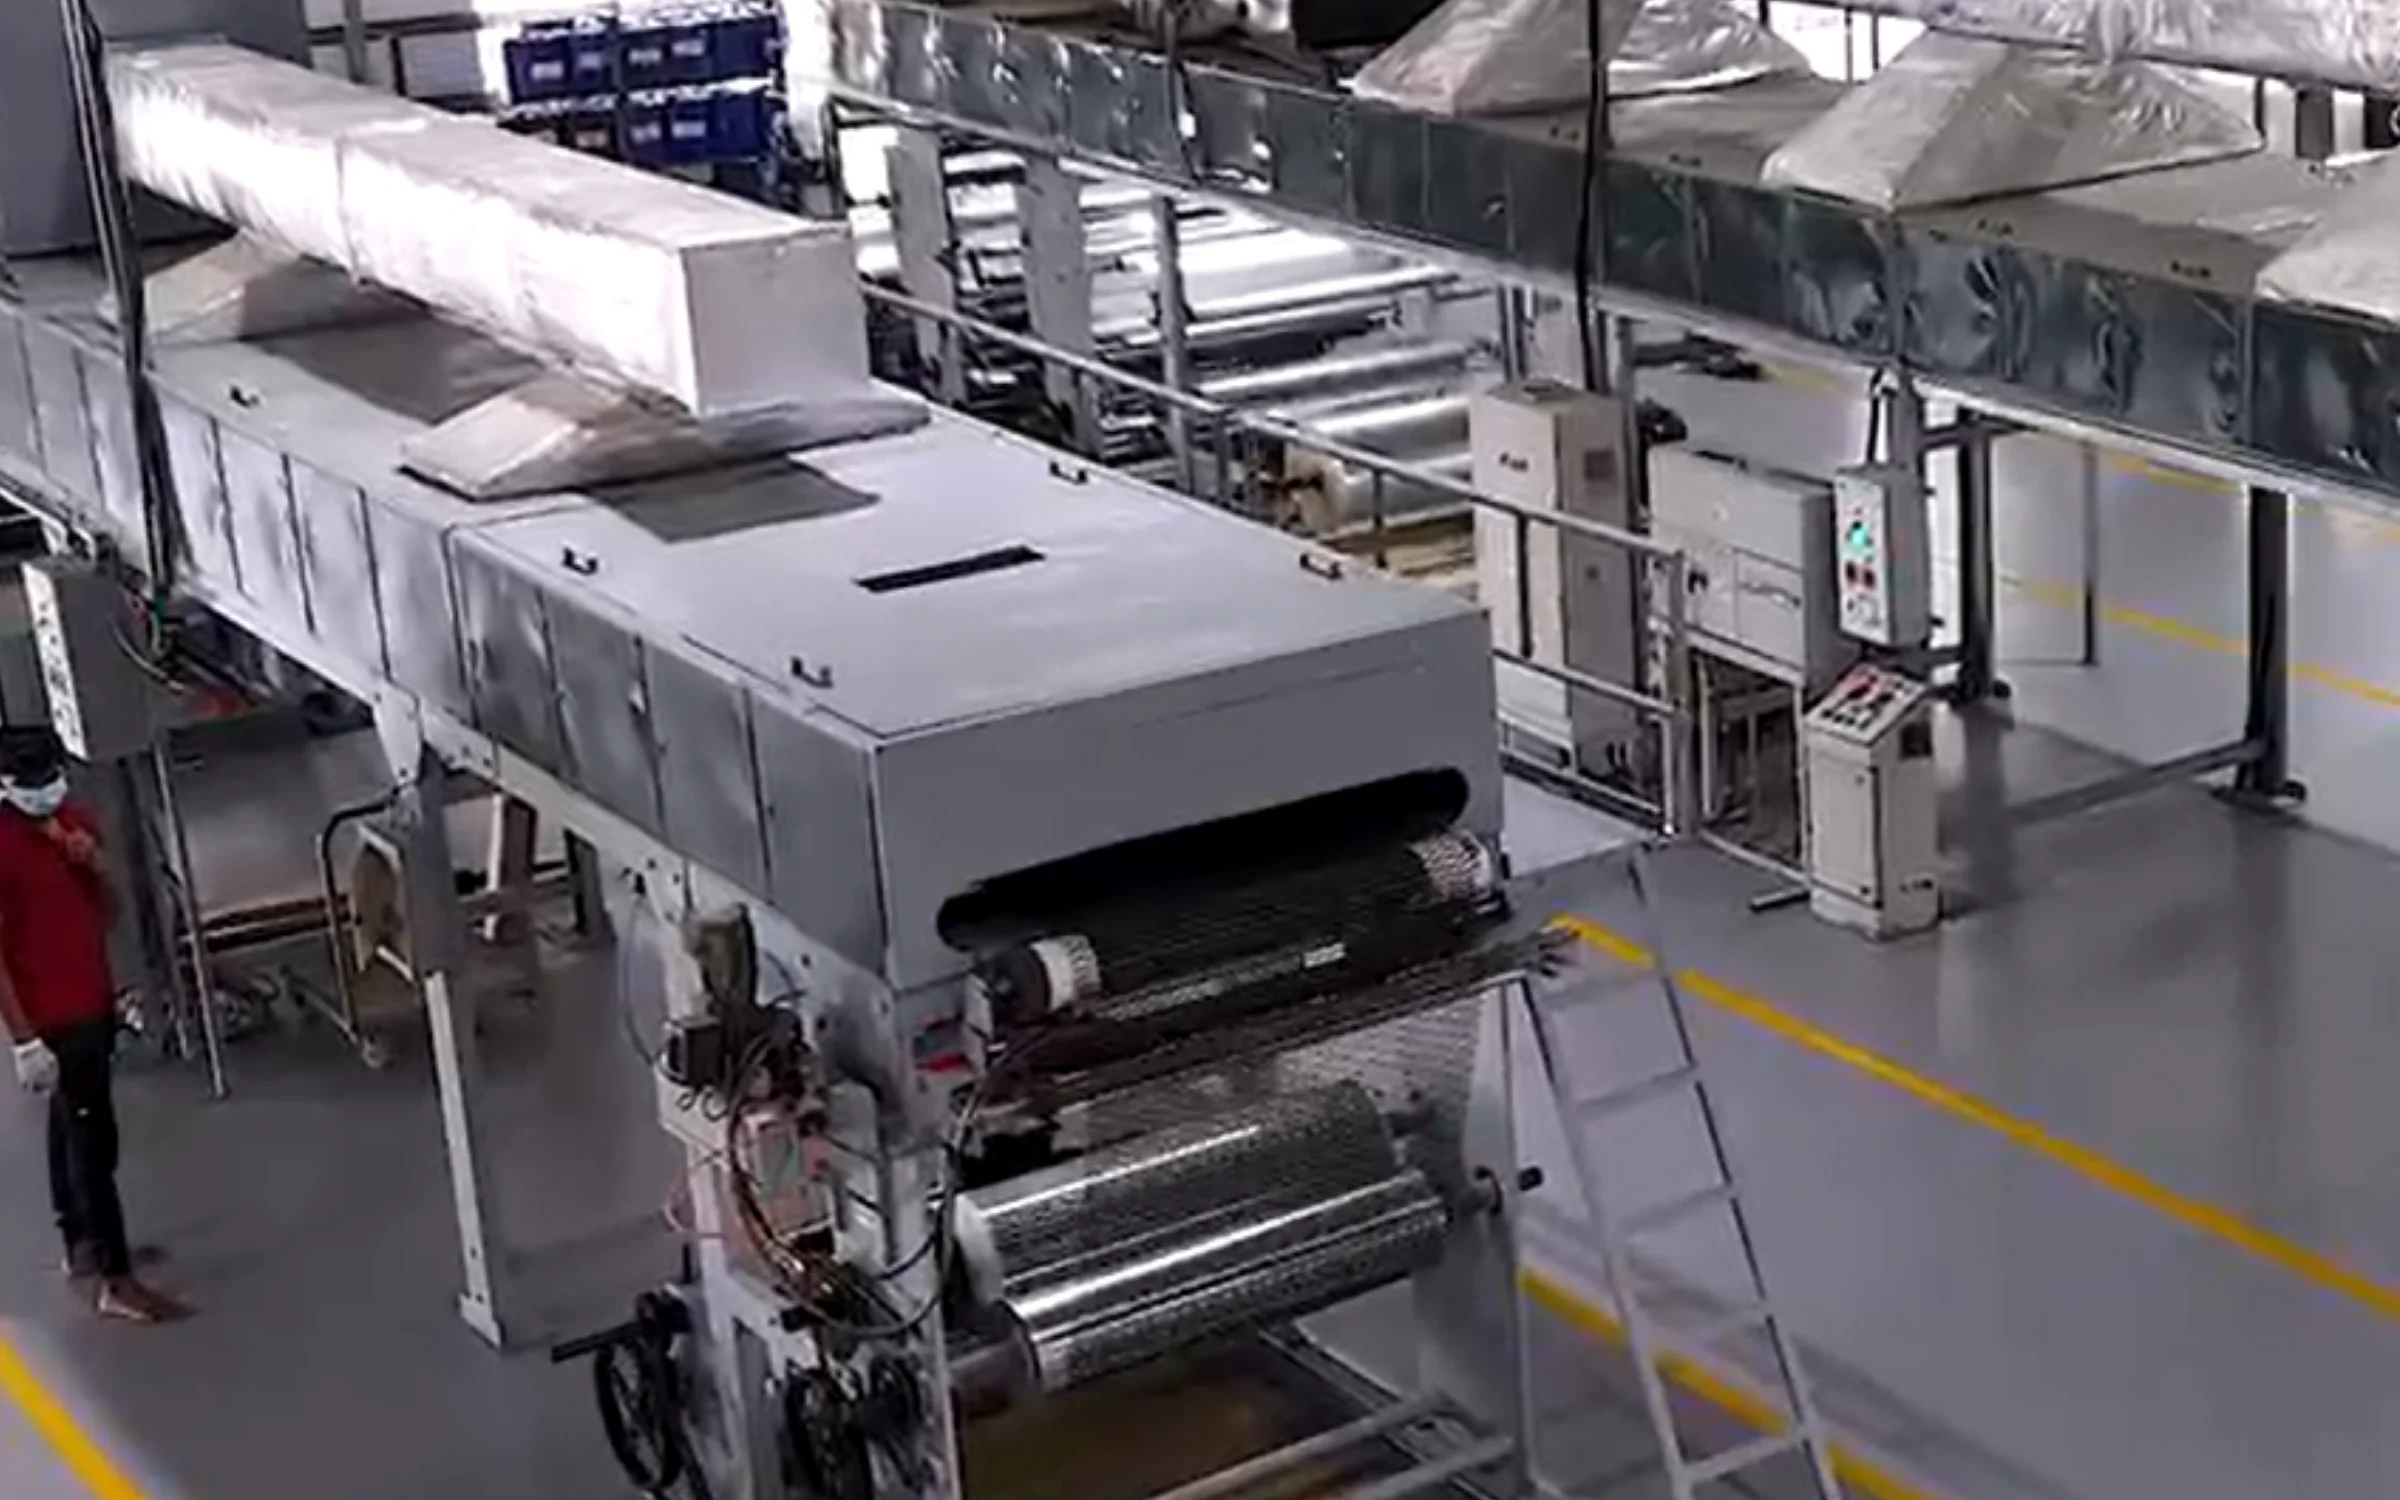
PLANT & MACHINERY
- Powered by three high-performance BOPP coating lines and seven ultra-precision slitter machines, our production ecosystem delivers flawless consistency and uninterrupted supply capacity.
- Enhanced with automated shrink-packaging systems and international-grade testing equipment, we meet and exceed global quality benchmarks.
- Our plant and machinery infrastructure is designed to support efficient, precise, and consistent adhesive tape manufacturing.
- Our machinery is configured to maintain accuracy across critical production stages, including coating, slitting, rewinding, and laminating.
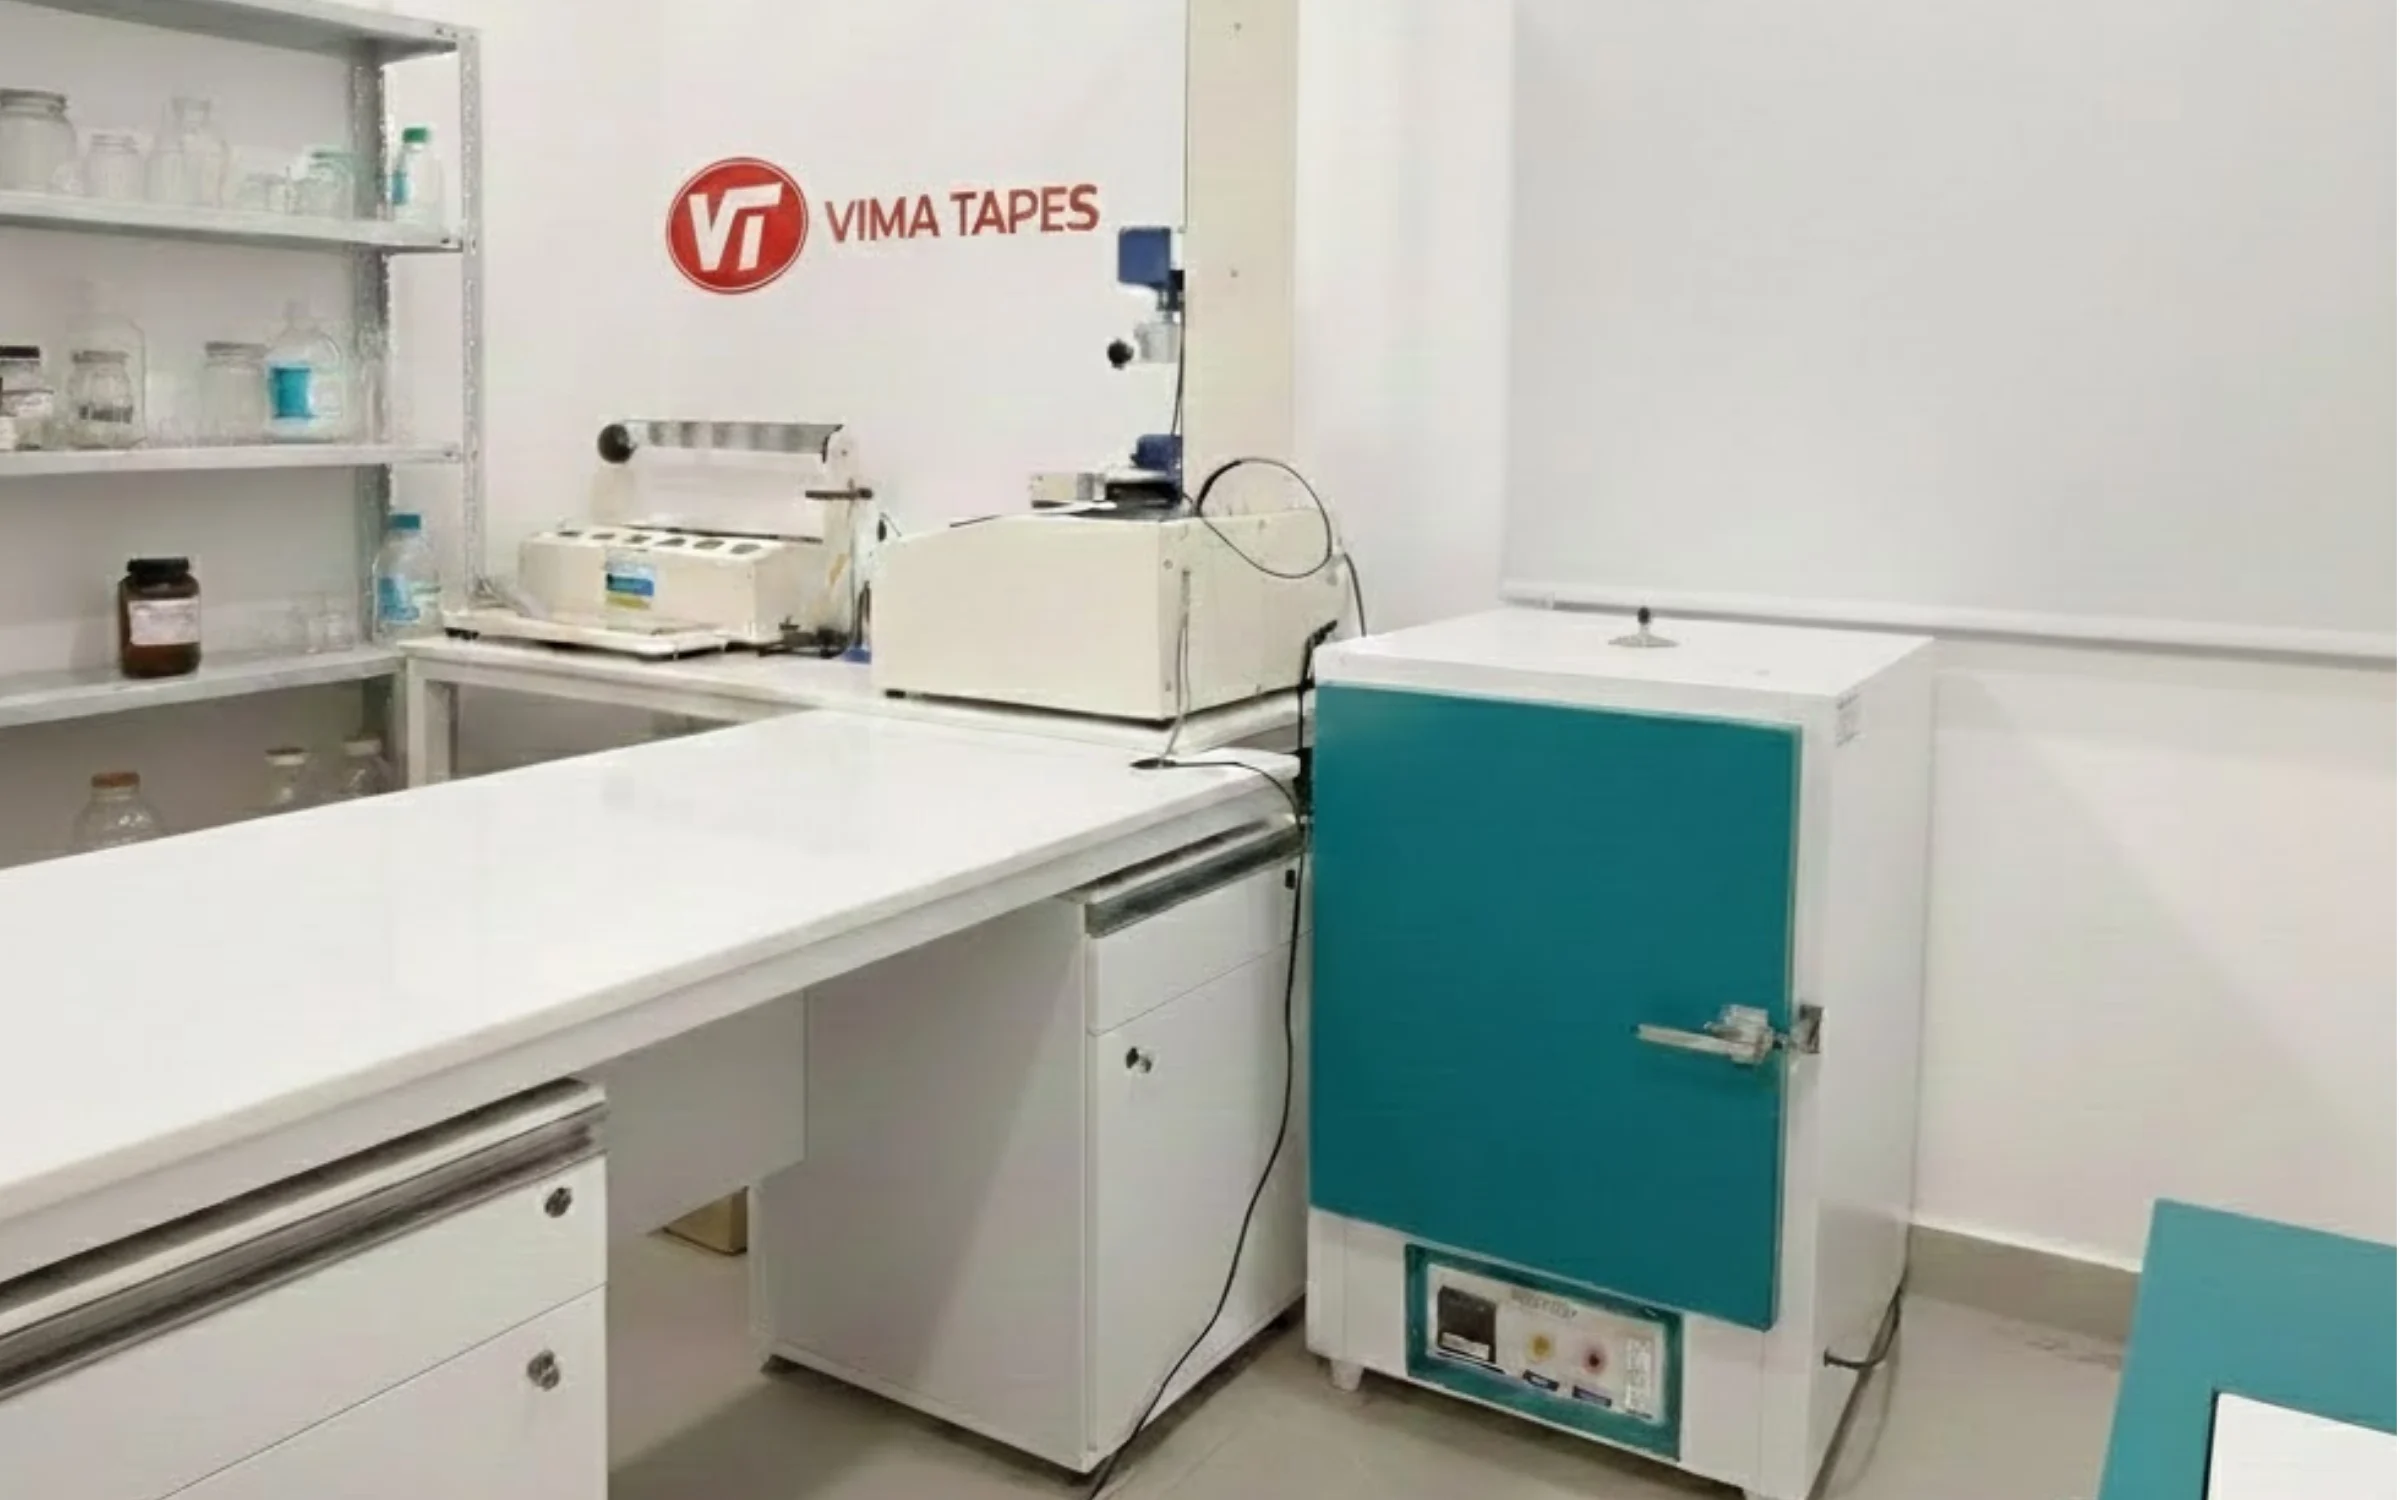
LAB FACILITIES
- Our fully equipped quality-assurance lab conducts a rigorous suite of tests to ensure every roll meets exacting performance standards.
- Assessments include Solid Content Strength, pH (Viscosity) analysis, Foaming evaluation, Peel and Shear Strength, Rolling Ball Adhesion, and Tensile Strength—ensuring consistent reliability, durability, and superior bonding across every batch.
- Our laboratory facilities support systematic testing and evaluation at different stages of product development and manufacturing.
- Products are evaluated against key performance parameters such as adhesion, tack, peel strength, thickness and tensile properties.
- Early-stage evaluation helps maintain consistency in manufacturing
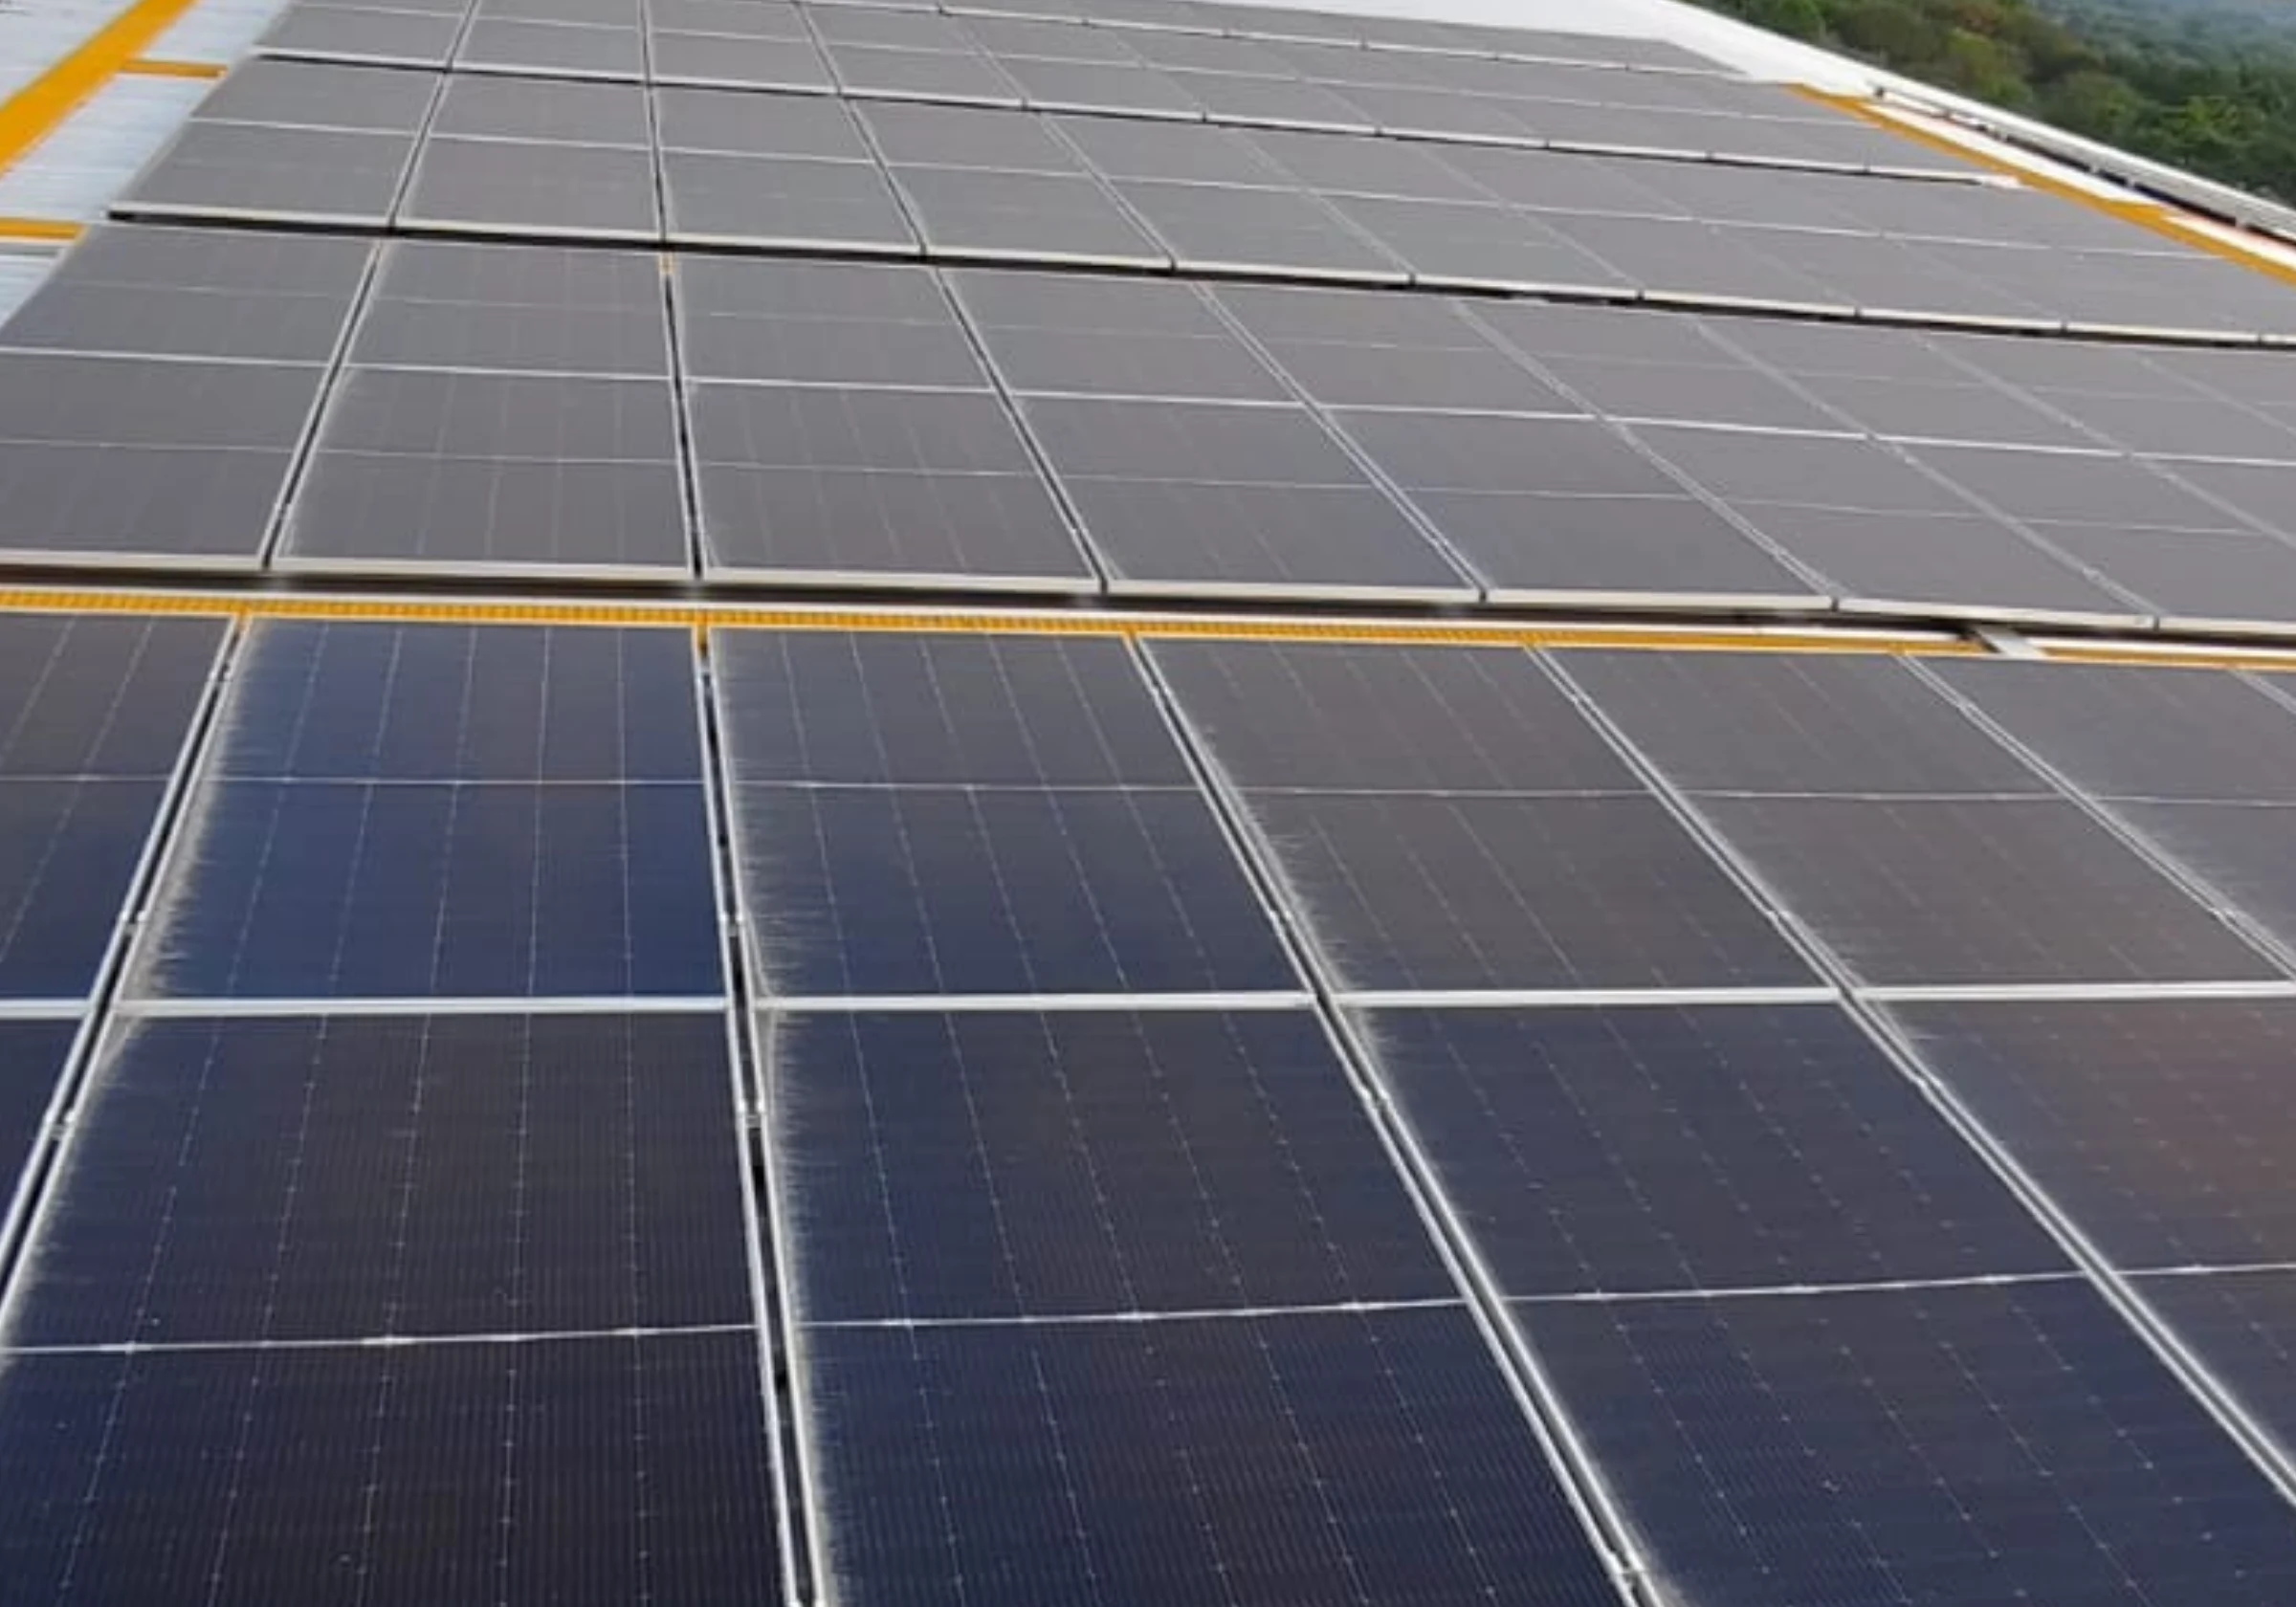
ENVIRONMENT
- Our in-house ETP enables responsible waste management and complete environmental compliance.
- A 100 kW solar installation powers a major share of our operations, significantly reducing our carbon footprint.
- Additionally, advanced scrubber systems ensure effective odor control and air pollutant filtration in line with regulatory standards.
- We continuously look for ways to optimise the use of raw materials, energy, water, and other resources throughout our operations.
- Better production planning, controlled operations, and systematic handling help us make more effective use of resources.
- We aim to incorporate environmentally conscious practices into our day-to-day manufacturing operations.
